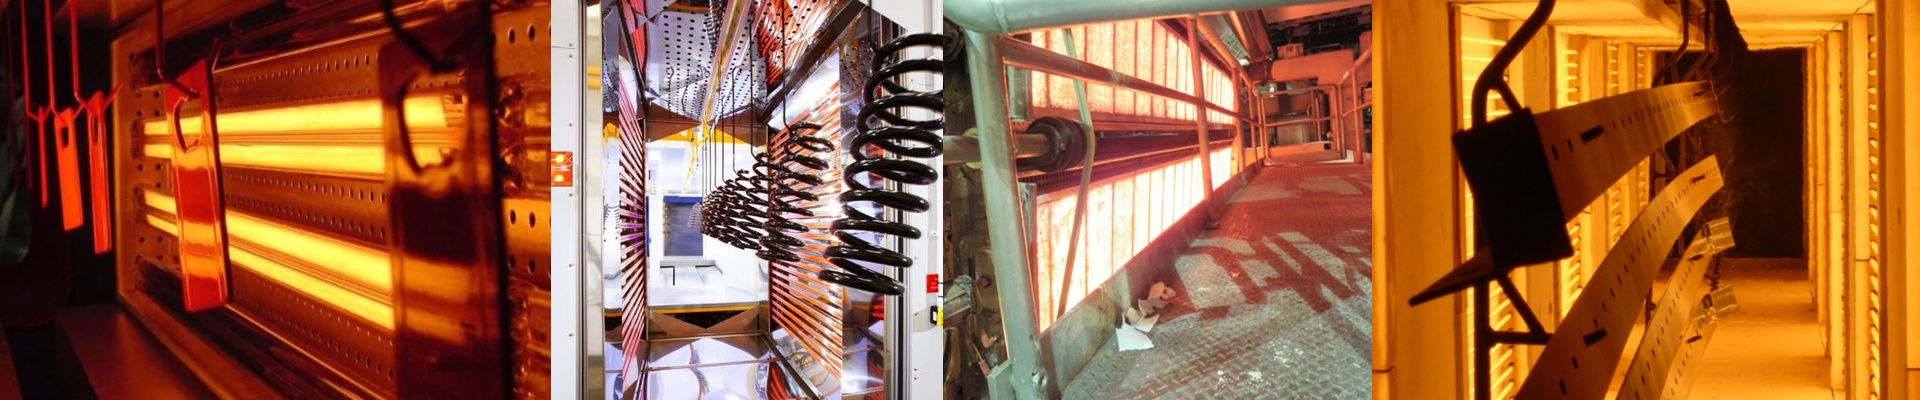
Getting Your IR Curing Right for Green Powder Coating
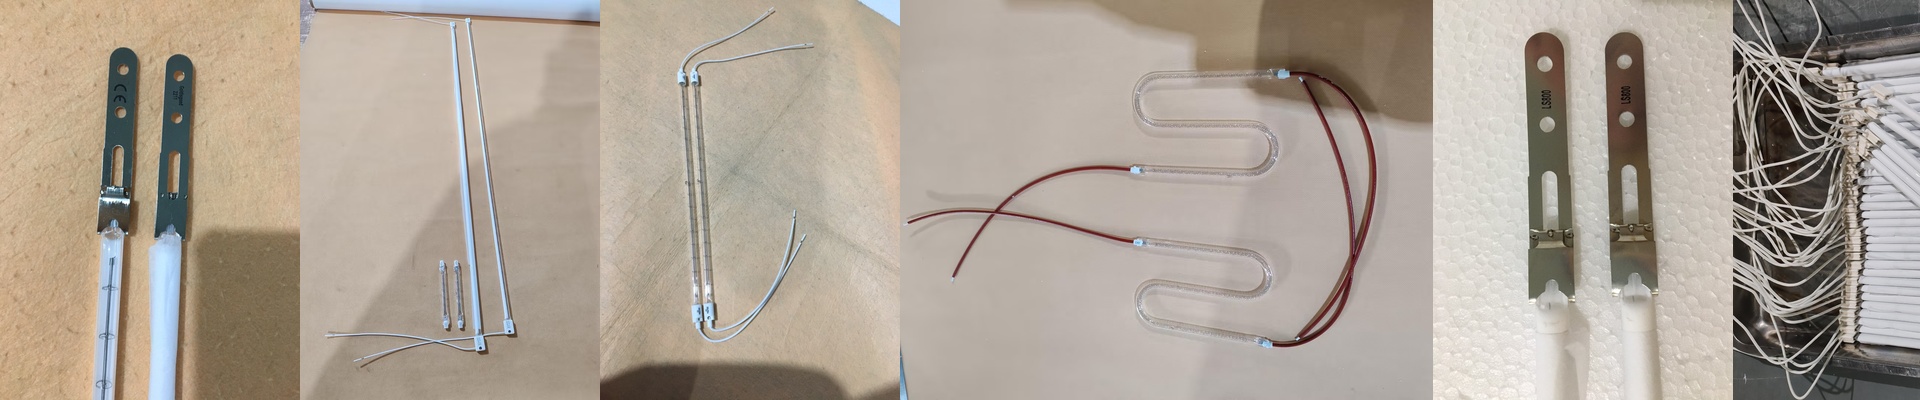
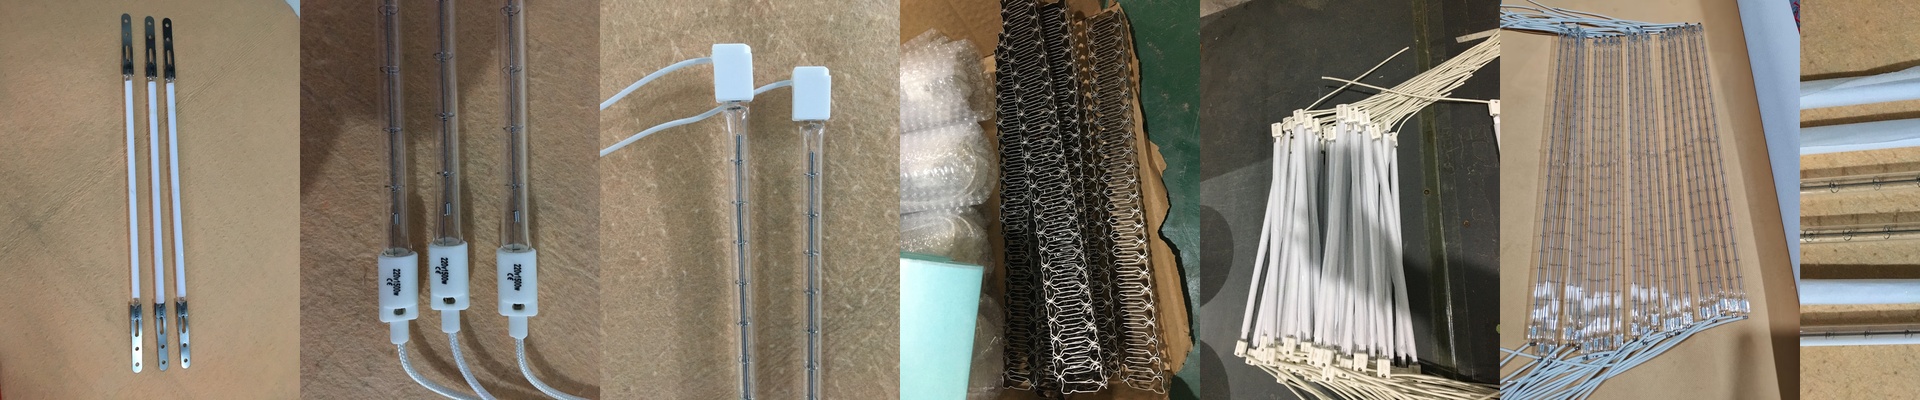
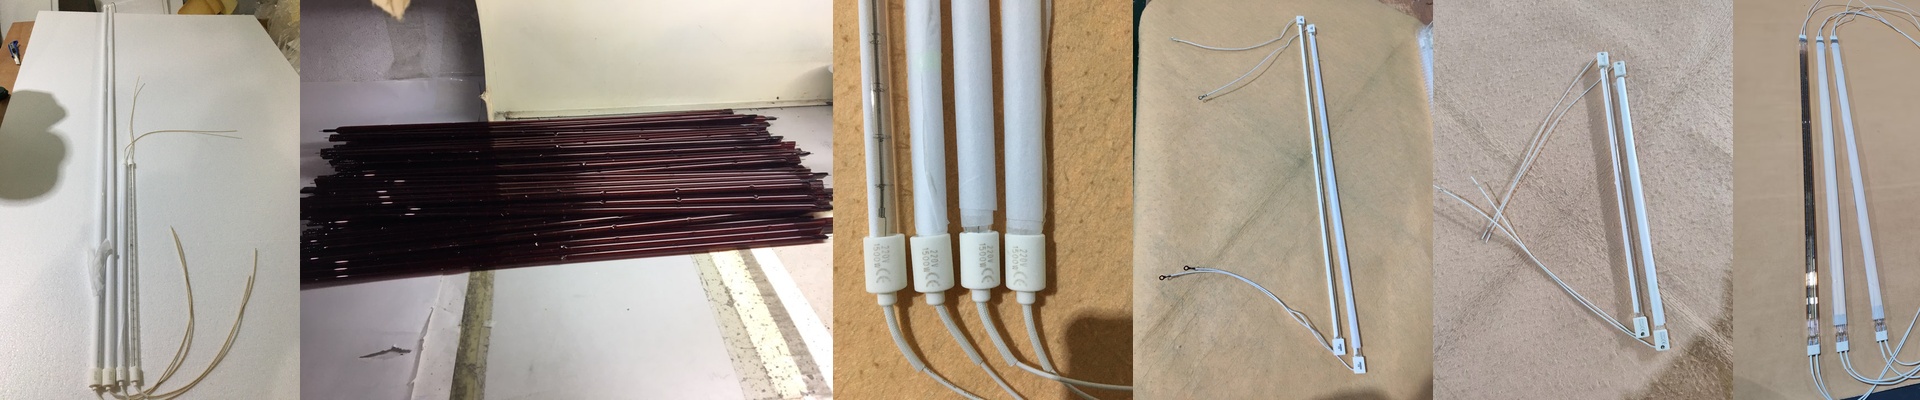
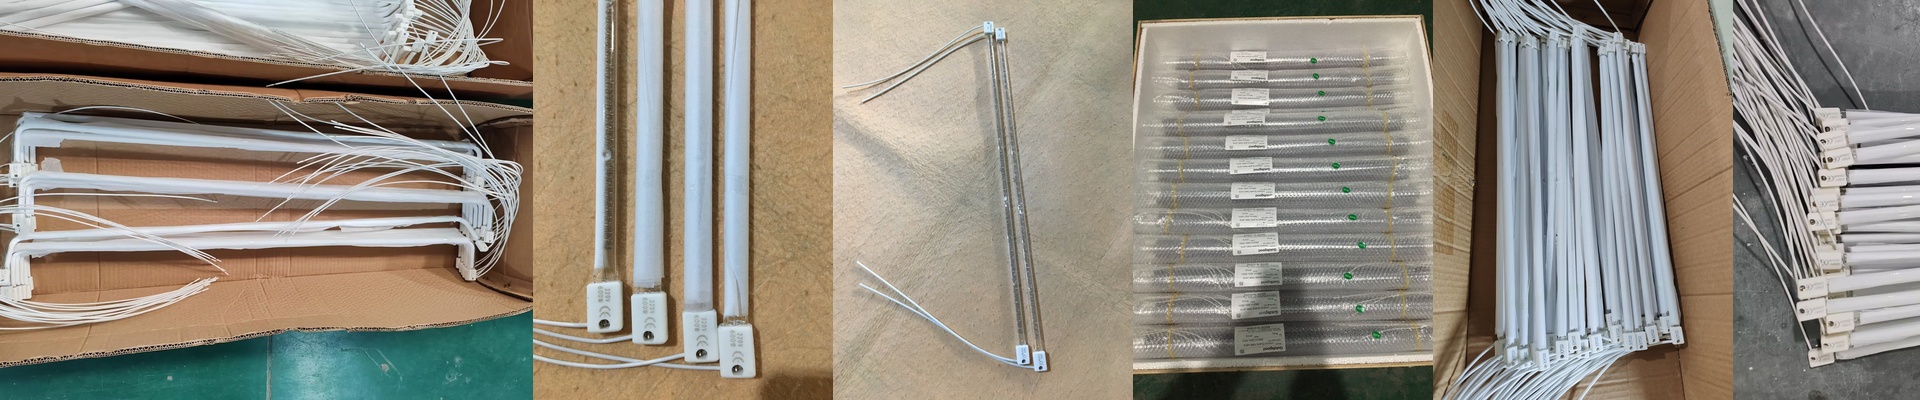
If you’re moving over to green powder coating, you already know the struggle. You need the heat to be exactly right. Too cold? The coating doesn’t bond. Too hot? You’ve just scorched your parts. We build our curing lamps to hit that sweet spot. If your current setup isn’t giving you the same rock-solid finish as the expensive, big-name brands, you’re probably dealing with under-curing. And that’s when the peeling starts. The heat side of things We load our tubes with high wattage so the heat actually penetrates the powder quickly. By using high-voltage setups, we can keep the lamps compact without losing any punch. The result? You get a concentrated heat zone that lets you speed up your conveyor. You move more parts, faster. Just a heads-up: when you’re pushing that much power, your reflectors have to be spot on. If they’re crooked, you’re just wasting electricity and risking hot spots that ruin the finish. Built for the real world Our lamps are made from high-purity quartz. Why? Because they need to handle the constant heating and cooling of a busy shop without cracking. We also use standard connectors. You can just pop these into your existing racks and get back to work. No need to spend your weekend rewiring the whole control panel. The real secret, though, is the spectral output. We’ve tuned these lamps to match the way powder resin absorbs heat. Instead of just warming up the metal substrate, the energy goes straight into the coating where it belongs. Shop floor reality Let’s be honest: factory gear takes a beating. You need something that just works. We’ve put our tubes head-to-head against the global leaders to make sure the results are the same. Because at the end of the day, the chemistry doesn’t lie. Either the powder cures or it doesn’t. If our lamps don’t perform exactly like the high-end brand you’re using now, we’ll give you your money back. Simple as that. Get the temperature right, and your finish stays put.